
| Metric | Result | Context |
|---|---|---|
| 10 | Major Components Installed | Four bent sections, three conveyor sections, one head section, one tail section, plus new belt frame and roller assemblies |
| 28 Days | Project Duration | Full installation completed inside a four week window at an operating cement plant |
| 40 | Personnel On Site | Approximately 40 personnel across multiple crews and simultaneous work areas |
| 20 Loads | Steel Delivered | Structural steel and conveyor components sequenced against the installation plan |
| 4+ | Concurrent Work Fronts | Laydown yard assembly, structural erection, belt frame and rollers, and head and tail sections advancing at the same time |
| Ahead | Schedule Performance | Completed ahead of the planned timeline |
| 0 | Safety Incidents | Project executed incident free |
Project Overview
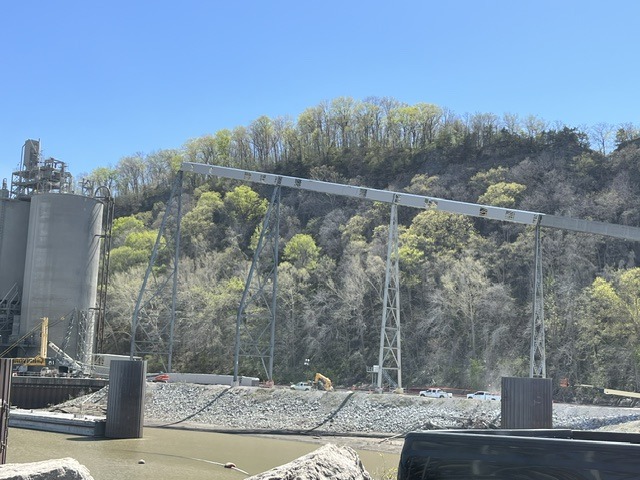
Southern Welding was engaged to install a new tube belt conveyor system and its supporting structural steel at the Holcim cement plant in Ste. Genevieve, Missouri, now operating as Amrize.
Ste. Genevieve is the largest single kiln cement plant in the world, producing roughly 4 million metric tons of cement a year. Work inside a facility of that scale happens on the plant’s terms, with site access and sequencing governed by an operation that does not stop for construction.
The scope covered ten major components: four bent sections, three conveyor sections, a head section, a tail section, and the new belt frame and roller assemblies. Roughly 20 loads of steel arrived over the course of the project, and approximately 40 personnel worked it across 28 days.
A tube belt installation is a chain of dependencies, and the conventional way to build one is sequentially, with each crew waiting on the one before it. Southern Welding ran it as parallel work fronts instead, and finished ahead of the planned timeline.
Component Specifications
| Component | Quantity | Scope |
|---|---|---|
| Bent sections | 4 | Assembled in laydown yard, erected on site |
| Conveyor sections | 3 | Installed within tube belt system |
| Head section | 1 | Installed and coordinated with structural sequence |
| Tail section | 1 | Installed and coordinated with structural sequence |
| Belt frame & roller assemblies | 1 | New frame and roller installation |
| Total major components | 10 |
Scope of Work
Structural Steel
- Installation of four new bent sections supporting the conveyor system
- Bent section assembly performed in the laydown yard, in parallel with site preparation
- Structural erection sequenced against material delivery
Conveyor Installation
- Installation of three conveyor sections within the tube belt system
- New belt frame installation
- Roller installation, run concurrently with belt frame work
Head & Tail Sections
- Installation of one head section
- Installation of one tail section
- Sequencing coordinated with the broader structural and conveyor scope
Multi-Crew Parallel Execution
A tube belt installation is a sequence of dependencies. The default approach is one crew finishing before the next begins, which means the schedule moves only as fast as its slowest handoff.
Southern Welding ran it as parallel work fronts instead. One crew built bent sections in the laydown yard while another prepared the site for erection, so structural components were ready before they were needed rather than after. A third crew worked the new belt frame and roller installation while head and tail section work progressed separately.
Keeping four fronts productive at once is a planning problem before it is a welding problem. Each day the leadership team built a plan around current priorities, available resources, material deliveries, and what the other crews were doing, with safety expectations set before work started rather than reviewed afterward. With roughly 40 people spread across multiple areas, that daily coordination is what kept the fronts from colliding.
The objective was not to keep people busy. It was to make sure every crew had what it needed to succeed.
What Made This Exceptional
Ten Major Components in 28 Days
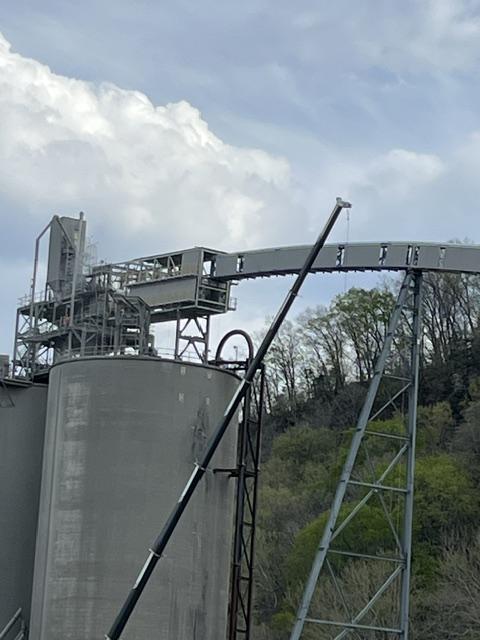
Four bent sections, three conveyor sections, a head section, a tail section, and the new belt frame and roller assemblies, all assembled and installed inside a four week window at an operating cement plant.
Parallel Work Fronts Instead of Sequential Handoffs
Dividing the work into concurrent workstreams let fabrication, structural erection, conveyor installation, and component installation advance at the same time. Progress in one area never depended on another area finishing first, which is where schedule is normally lost on a job like this.
Leadership Measured by Crew Success
Field leadership was organized around removing obstacles before they reached the crews. Each crew had a clear objective and the resources to meet it, and the daily plan was rebuilt around whatever the site actually required that morning.
Safety Built Into the Daily Plan
Safety was part of the daily planning conversation rather than a separate review. Crews started each day knowing the activities, the expectations, and how the work would be performed safely. Across 28 days, roughly 40 personnel, and multiple simultaneous work areas, that discipline is what made a productive project a safe one.
Results & Impact
| Component | Qty | Installation Scope |
| Bent Sections | 4 | Assembled in the laydown yard, erected on site |
| Conveyor Sections | 3 | Installed within the tube belt system |
| Head Section | 1 | Coordinated with the broader structural sequence |
| Tail Section | 1 | Coordinated with the broader structural sequence |
| Belt Frame & Roller Assemblies | 1 | New frame and roller installation, run concurrently |
| Total Major Components | 10 | Assembled and installed across 28 days |
The project delivered on its core objectives: safe execution, productive operations, and completion ahead of the planned timeline. By running multiple crews across coordinated work fronts, Southern Welding completed a complex tube belt installation faster than the schedule called for.
Delivered By
Southern Welding / AAA Fabrication
Project Manager: Tim Rolen
Delivered through the combined efforts of Southern Welding’s project management, field installation crews, fabrication personnel, tool room, and supporting team members.
Services Provided
- Structural Steel Erection
- Tube Belt Conveyor Installation
- Conveyor Frame Installation
- Roller Installation
- Bent Section Fabrication & Installation
- Head & Tail Section Installation
- Project Management
- Field Coordination
- Safety Planning & Execution
- Industrial Construction
The Southern Welding Difference
The Ste. Genevieve tube belt project shows what is possible when planning, leadership, skilled crews, and safety are brought together from the start.
By dividing the work into coordinated fronts and giving each crew a clear and safe plan, Southern Welding held productivity across multiple areas of an operating plant while beating the planned timeline.
When the crew succeeds, the project succeeds. When the project succeeds, the company succeeds.
Have a Project Like This?
Southern Welding self performs structural erection and conveyor installation at plants across the country. Tell us what is on your schedule and we will tell you how we would run it.
[Contact Us] or call (469) 517-0410